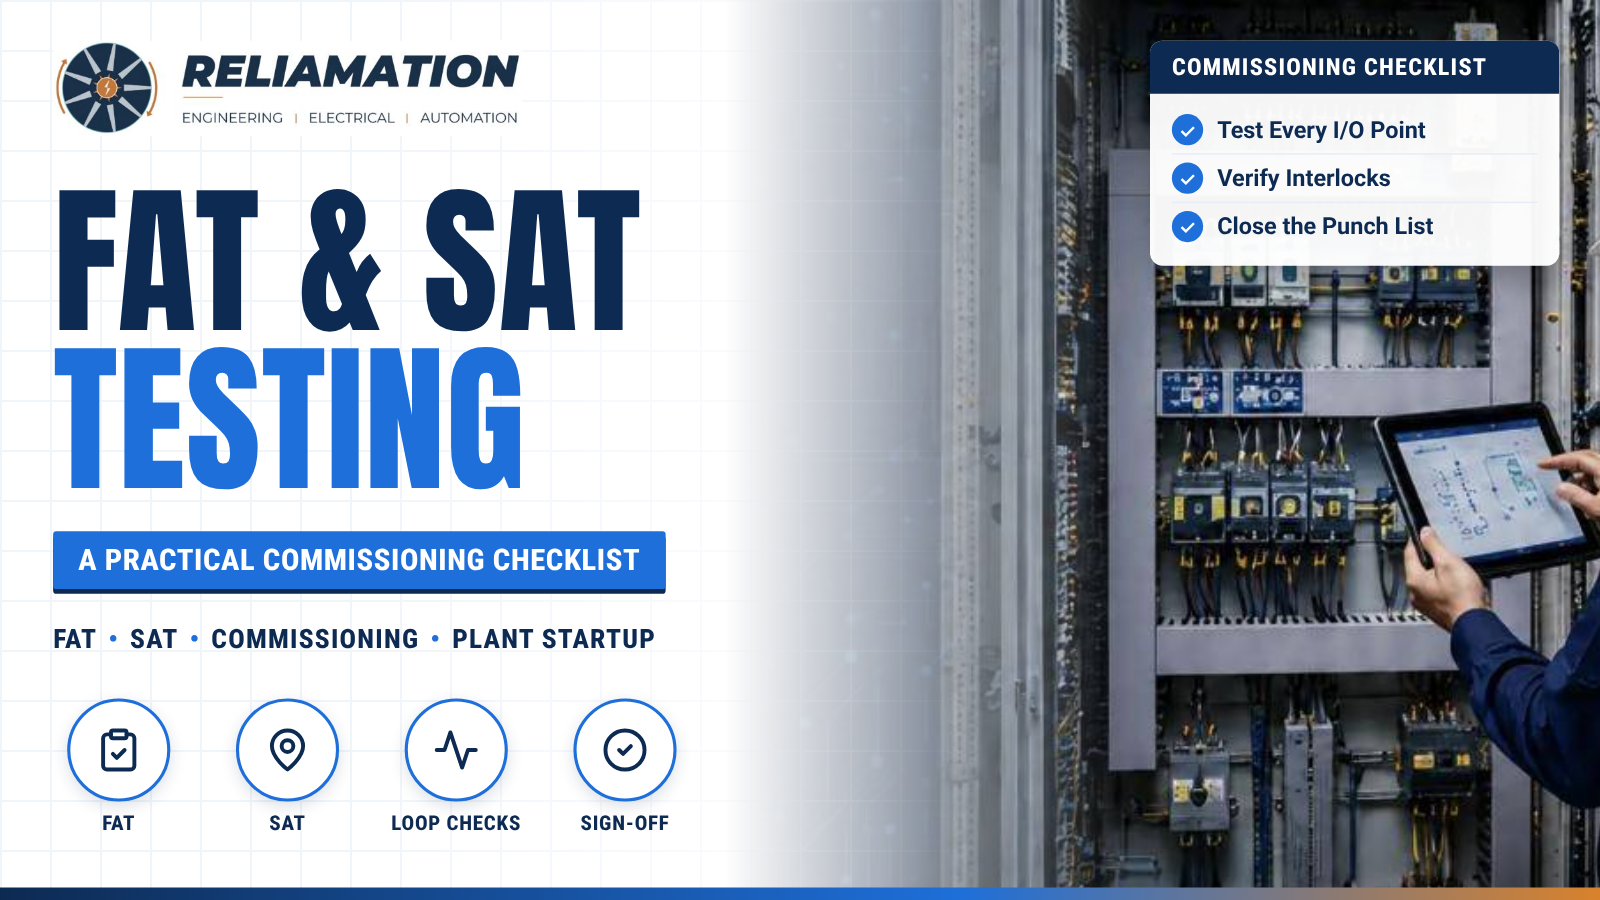
A new control system can look perfect on paper and still fail on startup day. Wrong I/O addresses, missing alarms and untested interlocks are often found too late, when the plant is waiting to run.
Two tests catch most of these problems early: the Factory Acceptance Test (FAT) and the Site Acceptance Test (SAT). The international standard IEC 62381 defines both tests for automation systems in the process industry.
This guide explains the difference between FAT and SAT and gives a simple checklist for each.
What Is a Factory Acceptance Test (FAT)?
A FAT is done before the system ships to site. The integrator or panel builder tests the control panels, PLC program and HMI screens with the owner present.
The goal is simple: prove that the system works as specified before it leaves the shop. Problems found here are faster and cheaper to fix than problems found in the field.
What Is a Site Acceptance Test (SAT)?
A SAT is done after the system is installed at the plant. It proves the system works with the real field devices, wiring, utilities and process conditions.
The SAT confirms what the FAT could not, such as real sensor signals, motor rotation, valve travel and communication with other plant systems.
FAT vs SAT: Key Differences
| FAT | SAT | |
|---|---|---|
| Where | Integrator’s shop or factory | Customer’s plant site |
| When | Before shipping | After installation |
| Field devices | Simulated | Real |
| Main goal | Prove the design and logic | Prove the installed system works in the process |
| Who attends | Integrator and owner | Integrator, owner, operators and maintenance |
FAT Checklist
- Approved drawings, I/O list and functional specification are on hand
- Panel inspection: labels, wiring, terminations and grounding
- Power-up and power-loss test
- Every I/O point tested with simulated signals
- Control logic and sequences tested against the specification
- Interlocks and permissives tested
- Alarms tested and alarm text checked
- HMI screens, navigation and user access checked
- Communication with drives, networks and other devices tested
- Punch list recorded and signed off
SAT Checklist
- Installation check: panels, field wiring and grounding
- Loop checks from field device to HMI
- Motor rotation and valve stroke checks
- Instrument ranges and scaling confirmed
- Safety functions and emergency stops tested
- Integration with SCADA, historian or other plant systems tested
- Sequences tested with the real process
- Operator training completed
- Final program backups saved
- As-built drawings and documents handed over
Tips for a Smooth FAT and SAT
- Agree on test procedures early. Both sides should approve the test plan before the FAT.
- Bring operators to the FAT. They catch HMI and workflow issues engineers often miss.
- Keep one punch list. Track every open item from FAT to SAT in one place.
- Do not skip the SAT. A good FAT does not prove field wiring or real process behavior.
- Back up at the end. Save the final PLC and HMI programs after the SAT, not before.
How Reliamation Can Help
Reliamation supports projects from design through startup. Our team handles FAT, SAT, loop checks, commissioning and operator training for plants in Texas and beyond. See our Plant Start-up & Commissioning services.
Need Help Planning a Plant Startup?
Contact Reliamation to talk about your commissioning plan.
Frequently Asked Questions
Get answers to common questions about industrial automation, PLC migration, HMI, SCADA, and control-system integration.
Reliamation provides industrial automation services including PLC programming, HMI and SCADA development, control system integration, legacy control-system migration, industrial networking, data reporting, system troubleshooting, and automation modernization.
Yes. Reliamation helps manufacturers migrate legacy platforms such as PLC-5 and SLC 500 to modern ControlLogix and CompactLogix systems while minimizing production disruption and preserving essential control functionality.
A PLC controls machines and industrial processes, an HMI allows operators to interact with equipment, and a SCADA system provides plant-wide monitoring, control, alarms, historical data, and reporting.
Yes. Reliamation develops custom HMI and SCADA solutions designed around each facility’s equipment, operating requirements, alarm strategy, security standards, and reporting needs.
In many cases, yes. A phased modernization approach can retain compatible equipment while replacing obsolete controllers, communication networks, operator interfaces, and other high-risk components.
Reliamation’s automation and control-system solutions can support manufacturing, food and beverage, plastics, packaging, material handling, water treatment, energy, and other process-driven industries.
Industrial automation can reduce downtime through reliable controls, real-time alarms, equipment diagnostics, historical data, preventive-maintenance insights, and faster troubleshooting.
You can contact Reliamation through the website to discuss your existing control system, operational challenges, modernization requirements, and project goals with an industrial automation specialist.