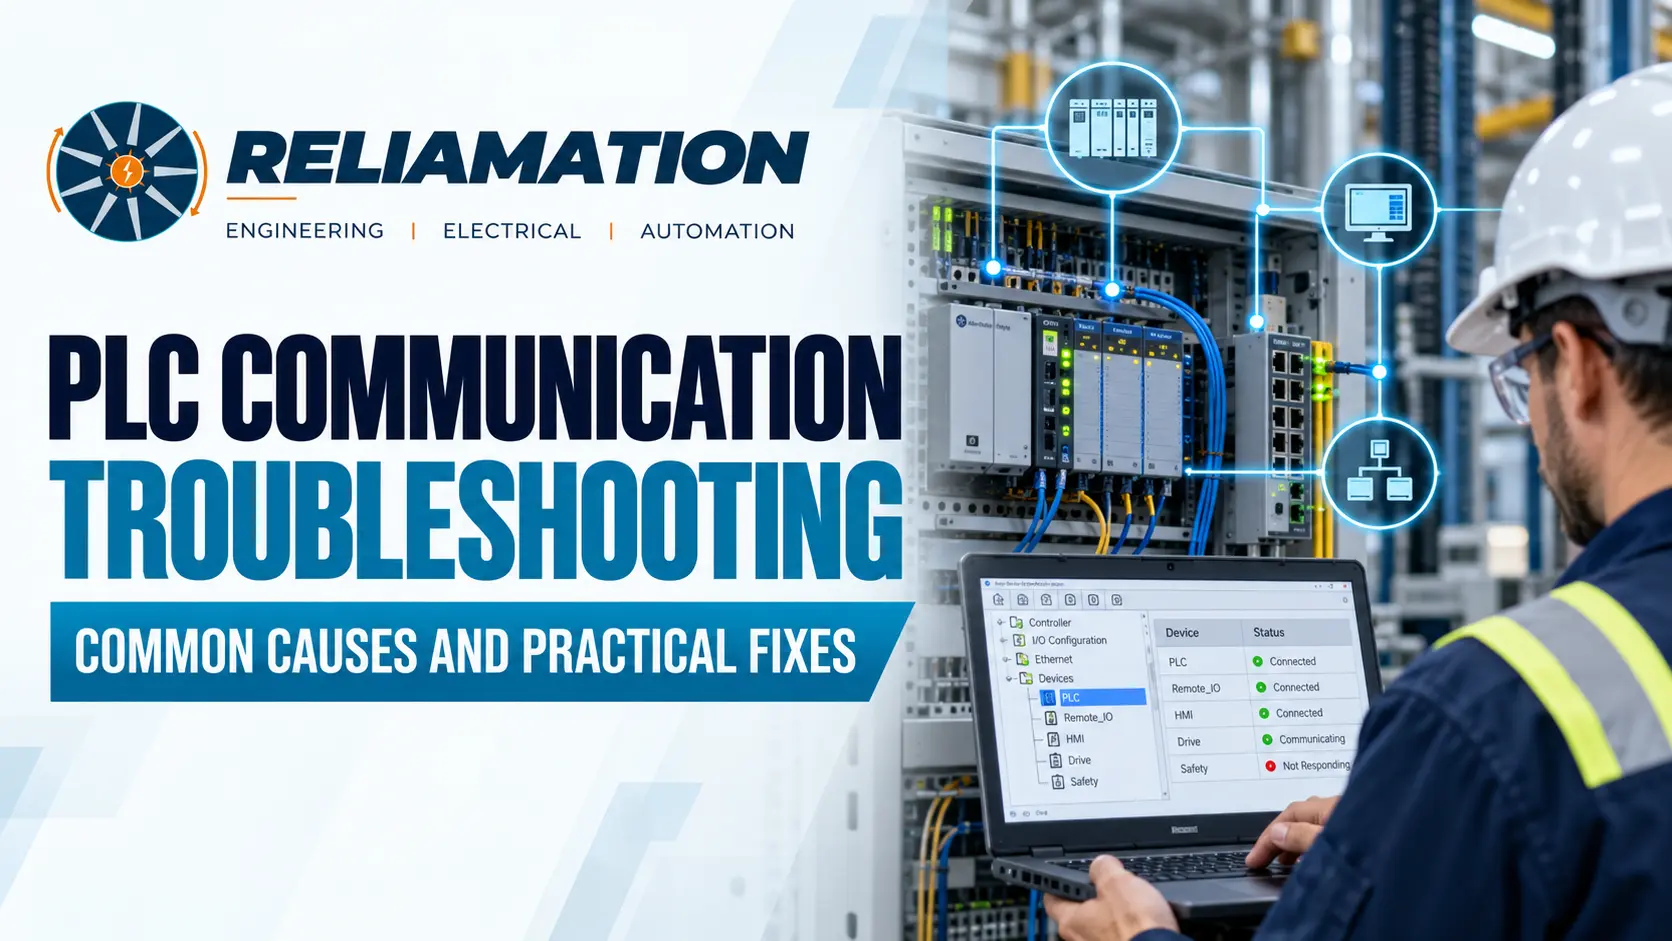
PLC communication problems can stop machines, disconnect HMIs, interrupt SCADA data, create remote I/O faults, and cause drives or other devices to disappear from the control system.
However, the device showing the alarm is not always the actual source of the problem.
An HMI may display “PLC Disconnected,” but the issue could be caused by a damaged Ethernet cable, an incorrect IP address, a wrong communication path, a switch-port fault, or a protocol configuration error. In the same way, a PLC may show a remote I/O fault even though the controller itself is operating normally.
For this reason, effective PLC communication troubleshooting should follow a logical process. Instead of rebooting equipment repeatedly or changing several settings at once, engineers should first understand the communication path and then work through the problem step by step.
Start With the Communication Path
The first step in PLC communication troubleshooting is to identify which two devices are supposed to communicate.
For example, the communication path may be:
HMI → Industrial Switch → PLC
or:
PLC → Industrial Switch → Remote I/O
or:
SCADA Server → OPC Server → PLC
Understanding this path helps narrow the problem quickly.
If one HMI cannot communicate with the PLC while another HMI remains online, the PLC may not be the problem. The issue may exist in the affected HMI, its network cable, switch port, or software configuration.
Similarly, if several remote I/O devices fail at the same time, the problem may be located in a shared switch, communication module, or upstream network connection.
A clear communication path prevents unnecessary troubleshooting.
Check the Basics Before Changing Configuration
Many PLC communication faults are caused by simple physical or power-related issues.
Before opening engineering software, verify that the affected devices have stable power. Check the PLC processor, communication module, HMI, industrial switch, remote I/O adapter, VFD, or gateway involved in the communication path.
Also inspect status LEDs. Most industrial devices provide indicators for power, network link, activity, module status, and communication faults. These indicators can often reveal whether the problem is related to the physical connection or to the controller itself.
Next, inspect the communication cables.
Ethernet cables, fiber connections, patch cords, and connectors can fail because of vibration, heat, moisture, physical damage, or poor termination. A cable that looks normal can still have an intermittent internal fault.
When site procedures allow it, replacing a suspect cable with a known-good cable is one of the fastest ways to rule out a physical-layer issue.
Verify IP Addressing and Network Settings
Incorrect IP configuration is one of the most common causes of industrial Ethernet communication problems.
Check the PLC IP address, subnet mask, gateway, and network interface. Then compare those settings with the connected HMI, SCADA server, remote I/O, or drive.
For example, if a PLC uses:
192.168.10.20
and the HMI uses:
192.168.10.30
with a subnet mask of:
255.255.255.0
the devices are typically on the same subnet.
However, if the HMI is accidentally configured as:
192.168.20.30
communication may fail unless routing exists between the networks.
Duplicate IP addresses can create even more confusing problems. Two devices using the same address may connect and disconnect intermittently, respond unpredictably, or cause communication faults that appear to move between devices.
Therefore, IP addresses should be checked against the current network documentation rather than assumed to be correct.
When the Network Works but the PLC Still Does Not Communicate
A successful ping does not always mean PLC communication is healthy.
Ping confirms basic IP connectivity, but it does not verify the industrial communication protocol or application configuration.
For example, a PLC may respond to ping while an HMI still cannot exchange tags because the communication driver points to the wrong controller. A Modbus TCP device may be reachable while the register address is incorrect. A PROFINET device may have the correct IP address but the wrong device name.
This is why PLC communication troubleshooting must go beyond simple network testing.
If basic connectivity is healthy, review the PLC and application-level configuration.
Check the controller’s communication module, connection diagnostics, device paths, protocol settings, and any configured remote devices.
On the HMI or SCADA side, verify the PLC address, communication driver, controller path, tag mapping, and network interface.
Often, the network is working correctly while the application is simply trying to communicate with the wrong device or through the wrong path.
Common PLC-to-HMI Communication Problems
PLC-to-HMI communication failures are common because both the network and the HMI project must be configured correctly.
A typical fault may occur after a PLC replacement. The new PLC is connected to the network and responds correctly, but the HMI project still points to the old processor address.
Another issue can occur when an HMI application uses a communication shortcut or driver configuration that no longer matches the PLC project.
When troubleshooting PLC-to-HMI communication, verify both ends of the connection.
The PLC should be online and healthy, while the HMI should use the correct IP address, protocol, and controller path.
If the HMI displays process values but cannot write commands, review user permissions, tag access, or command mapping rather than assuming the entire connection has failed.
Common PLC-to-SCADA Communication Problems
SCADA communication introduces additional layers because the system may use an OPC server, communication gateway, historian, or middleware between the SCADA application and the PLC.
A SCADA system may show bad-quality tags even though the PLC itself is healthy.
Possible causes include an incorrect PLC address, stopped OPC service, communication-driver fault, tag-path error, firewall rule, or network routing issue.
Therefore, troubleshoot the connection in stages.
First verify that the PLC is reachable. Then confirm that the OPC or communication service can connect to the PLC. Finally, verify that the SCADA application is receiving the correct tags from that service.
Breaking the communication path into smaller sections makes the problem much easier to isolate.
Common EtherNet/IP Communication Problems
EtherNet/IP is widely used for PLCs, remote I/O, drives, and other industrial devices.
In these systems, a device can be physically reachable on the network but still fail to establish its cyclic I/O connection.
The issue may be caused by a mismatch in device configuration, input/output assembly, firmware revision, module identity, or connection parameters.
For example, replacing a VFD with a newer hardware revision may require updating the controller configuration before the PLC accepts the device.
If an EtherNet/IP device is online but not exchanging I/O correctly, review the controller module diagnostics and device configuration rather than focusing only on the Ethernet cable.
Common PROFINET Communication Problems
PROFINET uses device names as part of device identification.
This means a device can have the correct IP address and still fail to communicate if the configured PROFINET name does not match the engineering project.
This commonly occurs after replacing remote I/O, drives, or other PROFINET devices.
For that reason, PROFINET troubleshooting should include:
- Device power
- Ethernet connection
- IP address
- Device name
- Engineering configuration
- Controller diagnostics
The important point is that IP addressing alone does not confirm a correct PROFINET configuration.
Common Modbus TCP Communication Problems
Modbus TCP troubleshooting often requires checking both the network and the data mapping.
A connection may be established while the returned values are incorrect.
Typical causes include:
- Wrong register address
- Incorrect offset
- Wrong function code
- Incorrect data type
- Byte-order mismatch
- Word-order mismatch
- Wrong unit identifier
For example, the PLC may successfully connect to a Modbus device but display zero or unrealistic values because the program reads the wrong register.
Therefore, engineers should distinguish between a communication failure and a data-mapping failure.
The two problems may look similar on the HMI, but they require different fixes.
How to Troubleshoot Intermittent Communication Faults
Intermittent communication problems are usually more difficult than permanent failures because the system may operate normally for hours before the fault returns.
Possible causes include loose cables, unstable power, failing switch ports, electrical noise, duplicate IP addresses, overheating hardware, or excessive network traffic.
The best approach is to collect evidence rather than making random changes.
Record the exact time of the fault, which devices were affected, and what the plant was doing when the problem occurred.
Then review:
- PLC diagnostics
- Switch logs
- Alarm history
- Network error counters
- Device power
- Environmental conditions
Patterns can be extremely useful.
For example, if communication fails only when a large motor starts, electrical noise or grounding may be involved. If the fault occurs every few minutes, a duplicate IP address or unstable network link may be more likely.
Intermittent faults require patience and good documentation.
A Practical PLC Communication Troubleshooting Example
Consider a production line where an HMI suddenly displays “PLC Disconnected.”
The first reaction might be to restart the PLC.
However, a better troubleshooting process begins by checking whether the PLC is still running.
The PLC status LEDs are normal, and another engineering workstation can connect to it successfully.
That tells us the PLC itself is likely healthy.
Next, the HMI network cable is checked. The link LED is on, but the HMI cannot ping the PLC.
The switch configuration is reviewed and shows that the HMI port was recently moved to a different VLAN during network maintenance.
The root cause is not the PLC, the HMI application, or the Ethernet cable.
It is the switch-port VLAN configuration.
After the port is returned to the correct VLAN, communication is restored.
This example shows why structured PLC communication troubleshooting is more effective than restarting equipment or replacing hardware without evidence.
Review Recent Changes Before Replacing Hardware
When a communication system has been stable for months or years and suddenly fails, ask what changed.
Recent changes often provide the fastest clue.
Examples include:
- PLC replacement
- HMI replacement
- Switch replacement
- IP address change
- Firmware update
- New remote I/O
- Drive replacement
- Firewall change
- Network modernization
- Software update
A system that worked before a recent change should be compared carefully with its previous configuration.
This does not mean the change is always responsible, but it should be investigated early.
Replacing hardware before reviewing recent changes can waste time and money.
Avoid Changing Multiple Settings at Once
One of the most important troubleshooting practices is to change one thing at a time.
If an engineer changes the PLC address, replaces the cable, reboots the switch, and modifies the HMI driver simultaneously, communication may return but the real root cause remains unknown.
A better process is:
Observe the fault, make one controlled change, test the result, and document what happened.
This makes troubleshooting repeatable and prevents accidental configuration changes from creating new problems.
How to Prevent Future PLC Communication Problems
Reliable communication starts with good documentation and maintenance.
Industrial facilities should maintain current network diagrams, IP address lists, PLC backups, HMI backups, device configurations, firmware records, and switch configurations.
Communication health should also be reviewed during preventive maintenance.
For example, managed-switch error counters may show a deteriorating Ethernet connection before the device goes completely offline.
Similarly, repeated PLC communication alarms may reveal an unstable remote device long before production stops.
Good change management is equally important. Every approved network or controller change should be documented so future engineers know what changed and why.
Why PLC Communication Troubleshooting Matters
PLCs do not operate in isolation.
They depend on communication with HMIs, SCADA systems, remote I/O, drives, network switches, and other automation devices.
As a result, one communication failure can affect machine operation, operator visibility, production data, and plant diagnostics at the same time.
A structured PLC communication troubleshooting process helps engineers identify the actual root cause instead of replacing equipment unnecessarily.
More importantly, it reduces troubleshooting time and helps restore production with fewer uncontrolled changes.
How Reliamation Can Help
Reliamation provides PLC programming, HMI and SCADA development, industrial networking, control-system integration, troubleshooting, and automation modernization services.
When communication problems involve several layers of the control system, the root cause may exist in the PLC, HMI, network, remote device, or protocol configuration.
A structured engineering approach helps isolate the problem and restore reliable communication.
Experiencing PLC Communication Problems?
Contact Reliamation to discuss PLC, HMI, SCADA, remote I/O, industrial networking, and control-system troubleshooting requirements.
Frequently Asked Questions
What is PLC communication troubleshooting?
PLC communication troubleshooting is the process of identifying and resolving communication faults between a PLC and devices such as HMIs, SCADA systems, drives, remote I/O, and industrial network equipment.
Why can I ping a PLC but the HMI still cannot communicate?
Ping only confirms basic IP connectivity. The HMI may still have an incorrect communication driver, PLC path, protocol configuration, or application setting.
What causes intermittent PLC communication problems?
Common causes include loose cables, failing switch ports, duplicate IP addresses, unstable power, electrical noise, excessive network traffic, and hardware faults.
How do I troubleshoot PLC-to-HMI communication?
Check device power, cables, IP addresses, subnet settings, PLC status, HMI communication driver, controller path, and tag configuration.
Why does remote I/O go offline?
Remote I/O can go offline because of power loss, cable problems, switch faults, configuration errors, communication-module issues, or hardware failure.
Can an industrial switch cause PLC communication faults?
Yes. A failed port, incorrect VLAN, configuration error, power issue, or unstable link can interrupt communication between PLCs and connected devices.
What should I check for Modbus TCP communication issues?
Verify the device IP address, connection status, register address, data type, function code, unit identifier, and timeout settings.
What should I check for PROFINET communication issues?
Check device power, network connection, IP address, PROFINET device name, engineering configuration, and controller diagnostics.
Should I restart the PLC when communication fails?
Restarting the PLC should not be the first troubleshooting step. Check diagnostics, network status, fault messages, and recent changes before rebooting equipment.
What should be documented after a communication fault is fixed?
Document the affected devices, fault symptoms, root cause, corrective action, configuration changes, replacement parts, and final validation results.
Frequently Asked Questions
Get answers to common questions about industrial automation, PLC migration, HMI, SCADA, and control-system integration.
Reliamation provides industrial automation services including PLC programming, HMI and SCADA development, control system integration, legacy control-system migration, industrial networking, data reporting, system troubleshooting, and automation modernization.
Yes. Reliamation helps manufacturers migrate legacy platforms such as PLC-5 and SLC 500 to modern ControlLogix and CompactLogix systems while minimizing production disruption and preserving essential control functionality.
A PLC controls machines and industrial processes, an HMI allows operators to interact with equipment, and a SCADA system provides plant-wide monitoring, control, alarms, historical data, and reporting.
Yes. Reliamation develops custom HMI and SCADA solutions designed around each facility’s equipment, operating requirements, alarm strategy, security standards, and reporting needs.
In many cases, yes. A phased modernization approach can retain compatible equipment while replacing obsolete controllers, communication networks, operator interfaces, and other high-risk components.
Reliamation’s automation and control-system solutions can support manufacturing, food and beverage, plastics, packaging, material handling, water treatment, energy, and other process-driven industries.
Industrial automation can reduce downtime through reliable controls, real-time alarms, equipment diagnostics, historical data, preventive-maintenance insights, and faster troubleshooting.
You can contact Reliamation through the website to discuss your existing control system, operational challenges, modernization requirements, and project goals with an industrial automation specialist.